Explore our core research-driven services and finished dosage softgel contract manufacturing solutions developed for global pharmaceutical and nutraceutical innovators.
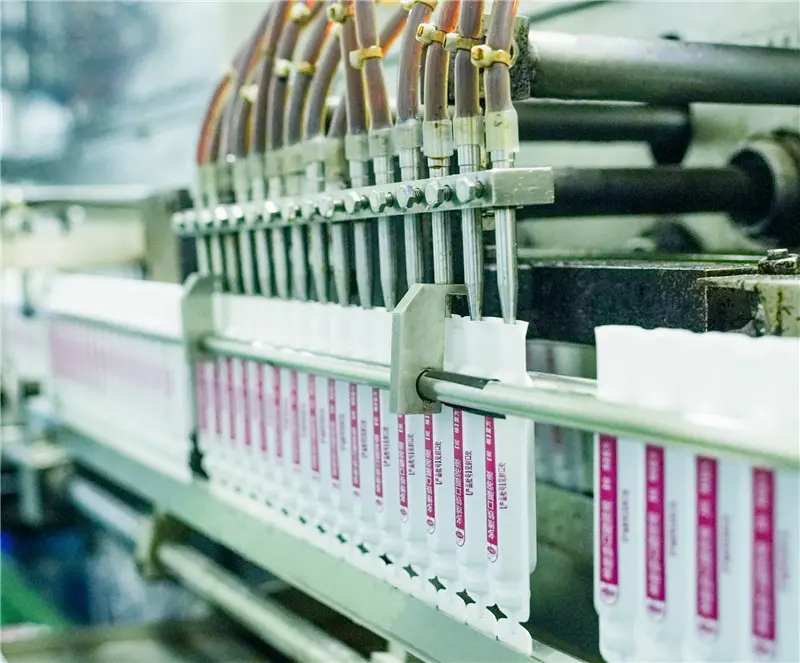
A comprehensive analysis of pharmacokinetic bioavailability enhancement, consumer swallowing adherence, and global regulatory scrutiny.
In modern biopharmaceutics and nutraceutical formulation engineering, the softgel capsule has transcended its traditional identity as a simple oil-carrier vessel. Today, soft gelatin and plant-based polymer encapsulation serve as an indispensable dosage form for BCS Class II (low solubility, high permeability) and BCS Class IV (low solubility, low permeability) molecules. Lipophilic bioactive compounds, botanical polyphenols, marine lipids, and fat-soluble micro-nutrients encounter severe oral absorption barriers in standard solid oral dosage forms such as tablets and dry-powder hard-shell capsules. Through micro-emulsification, Self-Emulsifying Drug Delivery Systems (SEDDS), and specialized co-solvent lipid formulation within a hermetically sealed elastic shell, softgels dramatically accelerate gastric dispersion kinetics, maximize intestinal micellar incorporation, and optimize systemic bioavailability.
Concurrently, the global procurement landscape has undergone a profound transformation. Institutional enterprise buyers, multinational consumer health brands, and pharmaceutical sponsors no longer evaluate an OEM Softgels Manufacturer & Supplier merely on machine speeds or basic unit pricing. The modern competitive benchmark requires demonstrated adherence to E-E-A-T (Experience, Expertise, Authoritativeness, and Trustworthiness) across the entire technological continuum. Procurement directors demand full supply-chain transparency, validated chromatographic profiling (HPLC/HPTLC), rigorously documented oxidation stability protocols, and verifiable compliance with US FDA 21 CFR Part 111/210/211, EU cGMP Annex 1, and international pharmacopeial harmonized monographs.
Encapsulation efficiency is governed by the physical chemistry of the fill matrix and the polymer shell's mechanical resilience. Minimizing plasticizer migration, avoiding cross-linking aldehyde reactions, and maintaining strict water activity levels (Aw < 0.45) are imperative to ensure a 36-month shelf life without shell brittleness or fill leakage.
By pre-dissolving hydrophobic botanical actives in customized lipid-surfactant carrier systems, softgels eliminate the rate-limiting dissolution step in human gastrointestinal fluids, facilitating rapid and uniform physiological uptake.
Polymer shells provide near-zero oxygen permeability when processed in inert nitrogen blanketed encapsulation zones, preserving vulnerable polyunsaturated fatty acids (EPA/DHA, Astaxanthin, CoQ10) from rancidity and active degradation.
Smooth, elastic softgel geometry significantly reduces swallowing friction and esophagus adhesion. Natural odor- and taste-masking properties ensure higher patient compliance in clinical regimens and consumer health brand loyalty.
Overcoming botanical cross-linking, moisture transfer, and formulation incompatibilities through cutting-edge chemical engineering.
Engineered utilizing high-purity tapioca starch, modified seaweed carrageenan, and vegetable glycerin. Delivers superior thermal stability in tropical climates (up to 45°C) without gelatin agglomeration, perfectly certified for Halal, Kosher, and Vegan markets.
Incorporating enteric polymers directly into the shell matrix eliminates the need for brittle post-coating. Protects acid-labile botanicals, live microbial ferments, and enzymes from gastric degradation while preventing fish-oil reflux and gastric irritation.
Proprietary homogenization systems permit stable suspension of insoluble active botanicals, micro-encapsulated beadlets, or dual-phase liquids within a single capsule, combining immediate-release and sustained-release pharmacodynamics without cross-reaction.
Botanical extracts rich in reactive polyphenols and aldehydes traditionally cause gelatin cross-linking and pellicle formation. We deploy chemically modified succinylated gelatin to guarantee rapid in vitro dissolution throughout extended real-time stability testing.
Strategic quality assurance matrices engineered to satisfy stringent multinational pharmaceutical audits and retail consumer mandates.
B2B contract procurement across North American, European, and Asia-Pacific markets is governed by uncompromising technical specifications. Global brand managers cannot afford batch rejections, product recalls, or non-conformance penalties. As a premier CDMO partner, MedGence aligns every stage of softgel development with International Council for Harmonisation (ICH) guidelines, providing thorough regulatory dossiers for New Dietary Ingredient (NDI) notifications, Traditional Herbal Medicinal Products (THMPD) compliance, and global pharmaceutical registration.
Full monograph testing adhering to USP, EP, and ChP standards: Shell seam thickness integrity analysis, fill weight uniformity (RSD < 2.0%), disintegration (< 30 mins in simulated gastric fluid), and residual solvent gas chromatography (USP <467>).
Equipped with closed-loop vacuum degasification and continuous nitrogen headspace sweeping to maintain Peroxide Values (POV < 5 meq/kg) and Anisidine Values (pAV < 20) for highly sensitive omega fatty acids and plant lipid extracts.
Automated ICP-MS screening for heavy metals (Lead < 0.5 ppm, Arsenic < 1.0 ppm, Cadmium < 0.5 ppm, Mercury < 0.1 ppm). Validated bio-burden control testing for total aerobic counts, yeasts/molds, and zero tolerance for E. coli, Salmonella, and S. aureus.
Harnessing automated cleanroom encapsulation lines, upstream agricultural integration, and rapid batch scalability.
The strategic advantage of China’s advanced pharmaceutical and nutraceutical manufacturing ecosystem lies in its comprehensive vertical integration. Located in Changsha, Hunan, MedGence operates at the geographical and logistical epicenter of China’s natural botanical production corridors. Unlike standalone Western contract packagers who purchase expensive raw active intermediates from overseas distributors, our facility provides unbroken supply chain custody: from native medicinal plant harvesting and standardized solvent extraction to pilot encapsulation and commercial-scale softgel production.
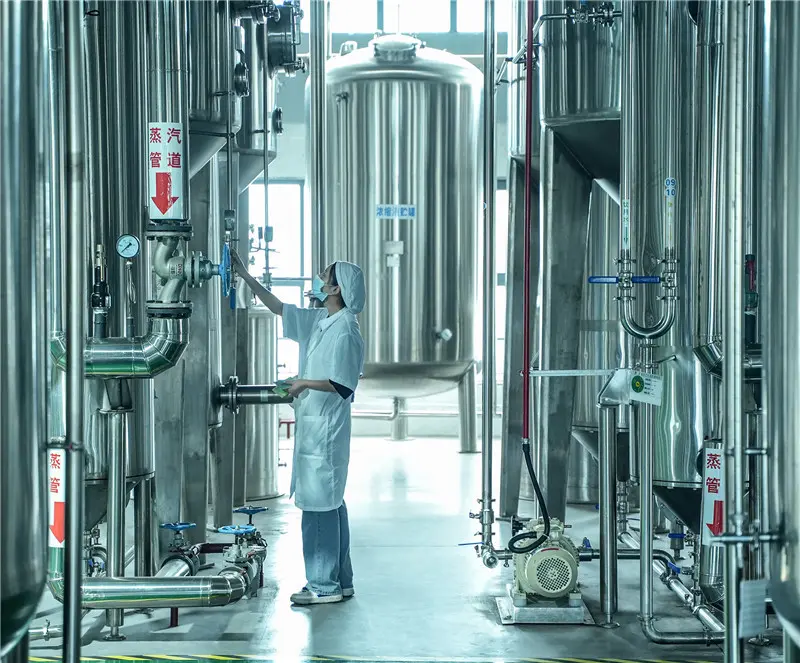
Our collaborative production factories integrate Industry 4.0 automation architectures. Fully closed-loop computerized gelatin melting systems, precision servo-driven rotary die encapsulation machinery, and intelligent vision-inspection sorters operate continuously inside ISO Class 7 (Class 10,000) cleanroom environments. Automated continuous-tumble drying tunnels linked to environmental SCADA systems regulate temperature (22°C ± 2°C) and relative humidity (20% ± 5%), mitigating the risk of case-hardening and ensuring optimal shell elasticity and seam fusion across millions of units per day.
Micro-calibrated die rollers ensure precise fill volume metering with micro-cavity tolerances under ±1.5%. Micro-grooved ribbon spreaders guarantee uniform gelatin thickness down to fractions of a millimeter.
High-speed 360-degree optical cameras automatically scan every single capsule on the conveyer line, eliminating 100% of physical defects including bubbles, seams, irregular geometries, or surface discoloration.
Direct sourcing of raw botanicals and automated high-throughput production translate into 30%–45% procurement cost reductions compared to Western contract packagers, accompanied by rock-solid lead-time stability.
14+ years of natural medicine research and industrial-scale formulation delivered for leading healthcare institutions.
From initial plant constituent screening to high-volume commercial finished product supply.
Deploying extensive phytochemical databases and state-of-the-art analytical equipment to isolate active alkaloids, polysaccharides, flavonoids, and saponins targeting specific therapeutic claims.
Quantifying active yield variances across geographical regions, harvest seasons, and plant tissues to establish an economical, high-potency raw botanical procurement baseline.
Developing validated assay methods utilizing HPTLC identification, HPLC quantification, GC volatile profiling, and multi-component chromatographic fingerprinting for rigorous batch consistency.
Engineering pilot-scale extraction, chromatographic resin purification, ultra-filtration, and low-temperature vacuum drying to ensure maximum active compound purity and extraction yield.
Formulating stable active lipid suspensions, resolving solubility deficits, neutralizing harsh tastes, and calibrating excipient compatibility to guarantee shelf-life integrity.
Conducting comprehensive safety dossiers including LD50 acute toxicity, sub-chronic toxicity, Ames testing, and in vivo genotoxicity testing to satisfy international health authorities.
Rapid screening utilizing enzymatic, receptor-binding, and cellular disease models to confirm pharmacological efficacy prior to animal or clinical investment.
Validating metabolic pathways, dose-response relationships, and systemic pharmacodynamics in rodent and non-rodent animal models to establish robust proof-of-concept.
Designing and managing GCP-compliant randomized, double-blind, placebo-controlled human clinical trials to substantiate structural-function claims and support New Drug Applications (NDA).
Modernizing classical Traditional Chinese Medicine (TCM) and complex multi-herb formulas into evidence-based, clinically validated modern pharmaceutical-grade delivery formats.
Supplying commercial quantities of standardized extracts, active botanical pastes, purified phytochemical powders, and natural volatile oils under strict GMP conditions.
End-to-end contract encapsulation: softgels, vegetarian capsules, oral liquids, tablets, and functional granules, packaged in bulk, blister packs, or bottled retail-ready formats.
Customizing encapsulation characteristics to align with specific end-user industry demands.
Prescription-grade natural formulations targeting cardiovascular support, hepatoprotection, and metabolic health. Standardized with rigorous chromatographic fingerprints and produced under GMP cleanroom conditions.
High-demand lipid formulations including Ultra-Pure Omega-3 Fish Oil, CoQ10 Emulsions, Vitamin D3/K2, Curcuminoids, and Saw Palmetto, encapsulated in gelatin or vegan carrageenan with transparent clean-label certification.
Unit-dose hermetic twist-off softgels designed for premium facial serums, antioxidant oils (Vitamin E, Bakuchiol, Astaxanthin), eliminating synthetic preservatives and preventing cosmetic oxidation upon storage.
Our validated CDMO research and encapsulation technologies underpin formulations for the nation’s most recognized healthcare entities.
 Beijing Tongrentang Group
 China Resources Sanjiu
 Sunflower Pharmaceutical
 Livzon Pharmaceutical
 Dihon Pharmaceutical
 Golden Throat Holdings
 Yangtzi River Pharma
 Beihai Gofar Biological
 Humanwell Healthcare
 SCIMYTH Pharmaceutical
 Shandong Hanfang Pharma
 Luoxin Pharmaceutical
 Zhongsheng Pharma
 Hunan Brilliance Medicine
 Apeloa Pharmaceutical
 Heng Chang Pharma Group
 Baotou TCM Co.
 Kamp Medicine
 Guangxi Santo Pharma
 Hunan Kangshou Pharma
 Jiangxi Juwang Pharma
 Beijing Tcmages Pharma
 Guizhou Ruihe Pharma
 Anhui CR Jinchan Pharma
 Kangmei Pharmaceutical
 Tianjicaotang Pharma
 Kingstone Unite Pharma
 Shuguang Hospital (Shanghai)
 Hunan Provincial TCM Hospital
 First Hospital of Hunan Univ.
 Second Xiangya Hospital
 Second Hospital of Hunan Univ.
 Orthopedics of TCM Zhuzhou
Comprehensive answers addressing regulatory documentation, encapsulation physics, MOQ parameters, and formulation feasibility.
Access precision testing, preclinical drug discovery, and large-scale contract encapsulation services.
Collaborate with our chief formulation scientists and pharmaceutical engineers to design, substantiate, and manufacture your next blockbuster softgel product.