Explore contract research, biological verification, and industrial manufacturing solutions designed to validate and optimize critical quality attributes.
Why modern biopharmaceutical and nutraceutical brand owners are shifting from generic procurement to tightly controlled Critical Quality Attributes (CQAs) and Critical Process Parameters (CPPs).
Global regulatory bodies (US FDA, EMA, NMPA) no longer accept simple post-production testing. Modern OEM/CDMO programs require proactive parameter engineering:
Natural raw materials suffer from significant variances caused by harvest seasonality, regional soil biochemistry, and processing methods:
Global brands face strict regulatory audits regarding heavy metals, solvent residue, pesticides, and microbial cross-contamination:
Combining classical botanical extraction knowledge with modern bioprocess automation to deliver unmatched commercial scaling velocity.
By housing analytical method development, extraction scaling, preclinical animal trials, and commercial dosage manufacturing under one technical umbrella, the typical transfer timeline is cut from 18 months down to under 6 months.
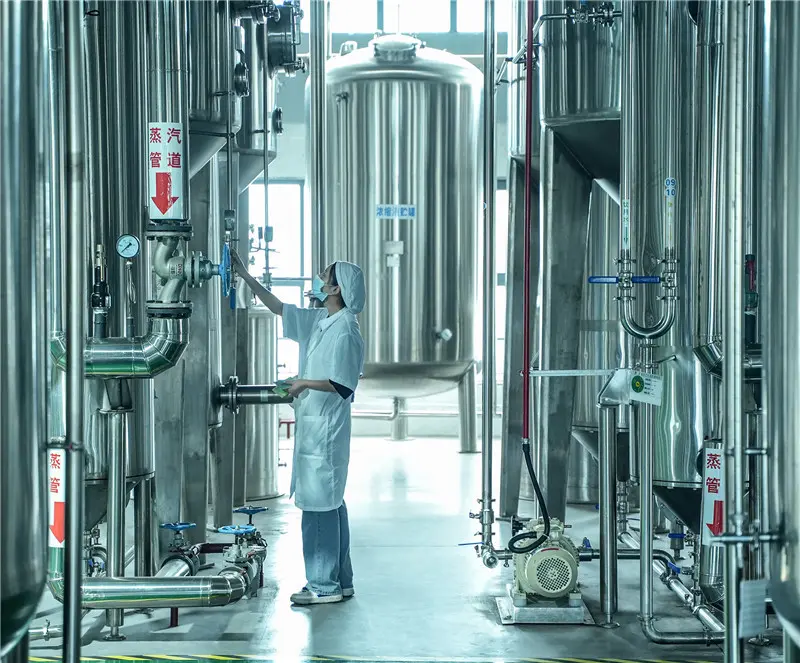
Our collaborative facilities feature multi-stage countercurrent extraction, supercritical fluid chromatography, low-temperature vacuum film concentration, and microencapsulation spray towers engineered to retain botanical potency.
Direct logistical connections to prime agricultural cultivation regions allow continuous multi-seasonal testing, selecting cultivars with the highest natural active ingredient ratios to lower overall processing mass requirements.
How precise parameters solve critical bioavailability, shelf-life, and sensory hurdles across various market verticals.
High-density granulations, microencapsulation for bad odor masking, moisture barrier optimization for softgel/capsule integrity, and rapid solubility profiles for functional effervescents and stick packs.
GMP-compliant Phase I-IV batch synthesis, impurity isolation, structural elucidation, validated stability chambers (ICH Q1A guidelines), and comprehensive toxicity testing frameworks.
Skin penetration optimization, reduction of heavy color pigments, oxidation-resistant emulsions, and sterile in vitro efficacy screening for anti-inflammatory and cellular regenerative claims.
Every industrial parameter is benchmarked against defined chemical analytical endpoints.
High-throughput identification of target alkaloids, polysaccharides, flavonoids, and active glycosides from multiple botanical species.
Method establishment using HPLC, HPTLC, and GC-MS fingerprinting to guarantee absolute batch-to-batch chemical conformity.
Determining critical ranges: thermal gradients, extraction pressure, solvent ratios, crystallization rates, and spray drying temperatures.
Execution of acute LD50 toxicity, sub-chronic toxicity assays, mutagenicity (Ames) tests, and cell-based biological assays.
Human efficacy validation, pharmacokinetic (PK/PD) studies, clinical data gathering for novel registration dossiers.
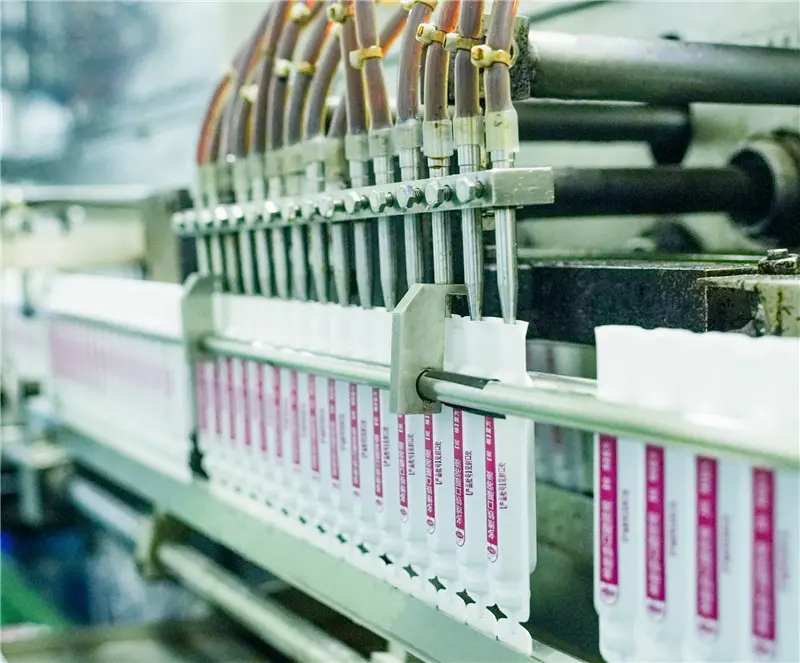
Turnkey packaging into finished forms: capsules, compressed tablets, oral liquids, softgels, granules, or bulk purified active powders.
The strategic shift in requirements from top pharmaceutical and health conglomerate procurement directors.
Modern clients demand full DMF (Drug Master File) components, complete stability data under stress conditions, and validated chromatographic standards that satisfy domestic inspections directly.
Entrusted manufacturing mandates rigorous intellectual property protection. Dedicated custom clean rooms, separated equipment trains, and enforceable contractual firewalls protect trade secret extraction methods.
Procurement teams increasingly require green extraction technology: zero-residue aqueous processing, supercritical CO2 fractionation, and zero-excipient formulations to satisfy consumer demands.
Detailed engineering and supply chain answers to help technical directors evaluate our CDMO platform.
A Critical Process Parameter is any variable whose variability impacts a Critical Quality Attribute (CQA). In natural active extraction, this includes solvent ratio, boiling points, column flow velocity, pH gradients during fractionation, and spray drying exposure times. Controlling these tightly guarantees batch-to-batch therapeutic bioequivalence.
Yes. We specialize in process scale-up. Our pilot plant models pilot yields against commercial equipment constraints, modifying hydrodynamic parameters and drying curves to ensure active molecules do not degrade when jumping from liter flasks to metric-ton extraction tanks.
We employ High-Performance Thin-Layer Chromatography (HPTLC) for qualitative botanical identity, HPLC and GC-MS for quantitative compound assays, and multi-wavelength UV or MS detectors for full chromatographic fingerprint verification against USP, EP, or ChP reference monographs.
All contract development operations are conducted under strict non-disclosure agreements (NDAs). Parameters developed specifically for client projects remain their exclusive intellectual asset, and physical manufacturing utilizes secured lines with full trace auditing.
We supply bulk raw active materials (concentrated liquids, ultra-fine powders, oleoresins, volatile oils) as well as primary and secondary packaged dosage forms including two-piece hard shell capsules, softgels, micro-tablets, effervescent tablets, oral syrups, and micro-granules.
Yes. In addition to Phase I-IV pharmaceutical protocols, we coordinate targeted, GCP-compliant small-group human intervention trials to establish credible, statistically valid structure-function data packages for premium consumer dietary supplement brands.
Select a core service line to consult with our technical formulation team or request custom batch specifications.