Comprehensive contract research services validated through over 14 years of scientific leadership, modern medical monographs, and proprietary pilot scale facilities.
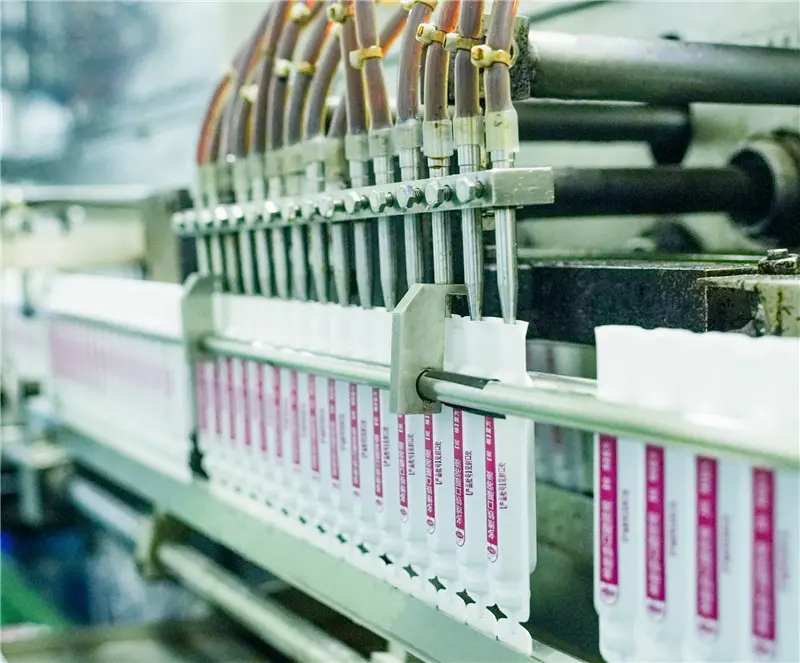
As regulatory environments shift toward carbon accounting and stringent impurity thresholds, traditional petrochemical solvents and high-emission extraction paradigms are being replaced by clean-label, low-emission bioprocessing.
The global pharmaceutical and wellness industry is undergoing an unprecedented regulatory and structural realignment. Heightened enforcement of environmental legislation—such as the European Union Corporate Sustainability Due Diligence Directive (CSDDD), EU Carbon Border Adjustment Mechanism (CBAM), and United States FDA clean-solvent thresholds (USP <467>)—demands that raw material synthesis and contract manufacturing evolve beyond simple price competition. Legacy extraction techniques that rely heavily on halogenated or volatile organic solvents (VOCs) like hexane and chloroform create toxic effluent footprints, consume excessive thermal energy, and leave undesirable chemical traces.
For cross-border brand owners, brand vulnerability is no longer limited to shelf life or microbial count. Regulatory authorities and institutional consumers audit the full Scope 1, 2, and 3 emissions across the botanical lifecycle. An ODM environmentally friendly manufacturer must resolve the friction between industrial throughput and ecological responsibility. Modern CDMO infrastructure replaces outdated batch processes with continuous counter-current extraction, subcritical water treatment, and supercritical fluid CO2 extraction to guarantee botanical purity without compromising environmental ethics.
Transforming raw botanical mass into pharma-grade bioactive fractions requires precise physical thermodynamics, membrane separations, and digital chromatographic auditing.
Utilizing dense-phase carbon dioxide at supercritical states allows tuneable selectivity for lipophilic molecules, volatile terpenes, and essential phytosterols without organic solvent residues. Combined with high-temperature subcritical water fractions, targeted bioactives are unlocked cleanly while thermal degradation of polyphenols and polysaccharides is minimized.
Traditional decolorization and thermal concentration often rely on carbon beds that generate solid waste, coupled with high steam usage. We employ cross-flow multi-stage ceramic nanofiltration and reverse osmosis modules. This enables nonthermal physical concentration, conserving up to 70% of processing energy while purifying sensitive compounds.
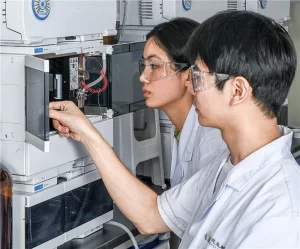
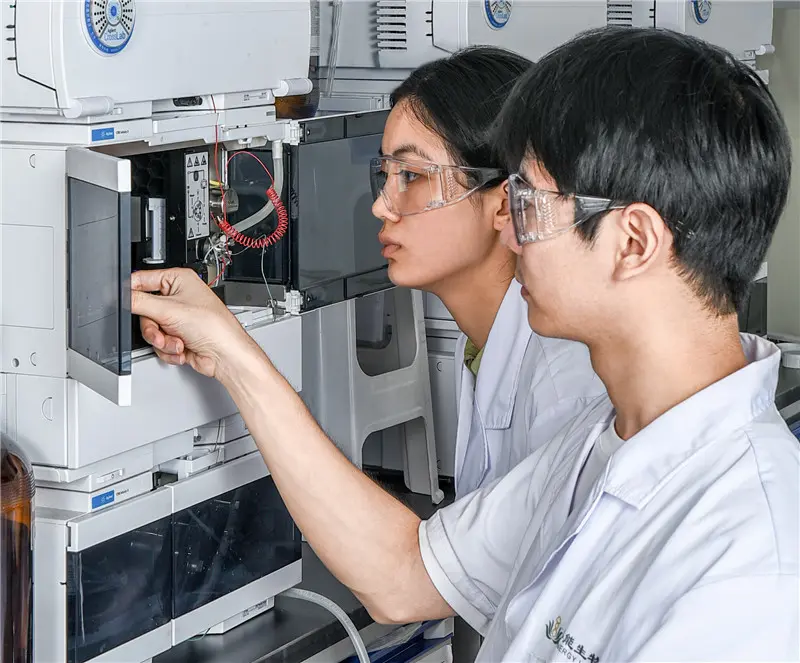
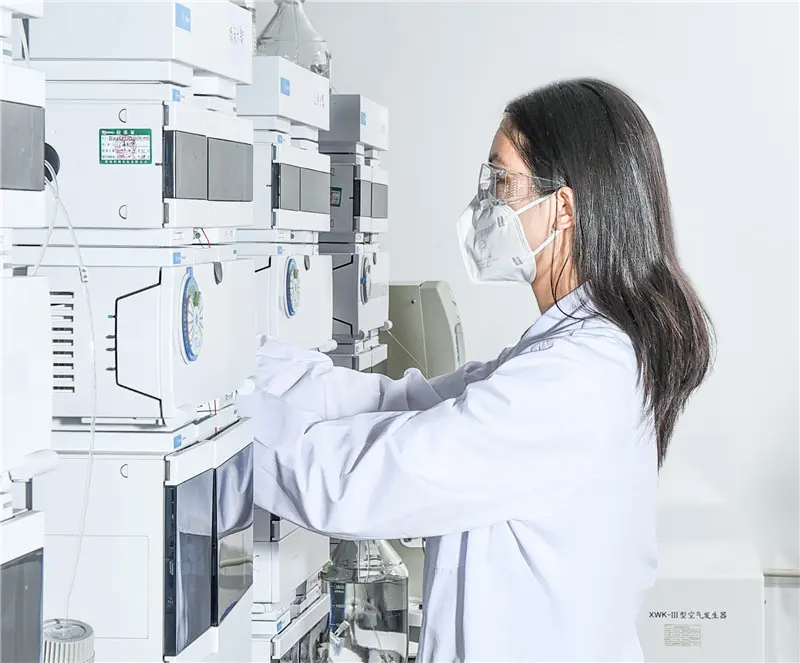
Every extract carries a unique phytochemical fingerprint. Integrating online HPTLC identification, HPLC-MS/MS, and automated gas chromatography lets us map the comprehensive bioactivity profile in real time. Machine learning algorithms model seasonal variations across growing regions, identifying the harvest windows that produce optimal active density.
With deep roots in Changsha, Hunan, our scientific team links traditional pharmacological wisdom with standardized analytical protocols and commercial production.
Years Dedicated to Natural Medicine CRO & CDMO
In-House Scientists, Pharmacists & QA Personnel
Top Pharmaceutical Groups & Hospitals Served
Classic TCM Formula Medical Studies Completed
Innovative Natural Botanical Medicines Developed
Hospital Preparation Drug Formulations Registered
Single-Herb Production & QC Processes Standardized
Formula Confidentiality & IP Protection Protocol
Translating botanical actives into shelf-stable, compliant, and consumer-ready formats tailored to jurisdictional preferences across North America, the EU, and Asia-Pacific.
We support dietary supplement leaders in meeting demands for bioavailability, organic certifications, and non-GMO claims. Our micro-encapsulated dry extracts and water-dispersible emulsions resist gastric degradation, providing clean-label actives for immune modulation, metabolic support, and cognitive clarity in powders, chewables, and softgels.
From single pure compound isolation to standardized multi-herb fractions, our laboratories generate preclinical packages compliant with ICH-Q7 guidelines. We validate batch-to-batch repeatability, characterize impurities, and conduct GLP-level toxicity assessments (LD50, acute, chronic, genotoxicity) to support your IND and NDA dossiers.
Modern personal care brands require alternatives to synthetic additives without sacrificing potency. We isolate skin barrier-repairing triterpenoids, soothing flavonoids, and antioxidant polyphenols. Validated via in vitro dermal models and cytokine assay panels, our actives meet EU Cosmetics Regulation 1223/2009 clean-label criteria.
Operating at the intersection of raw material access, industrial automation, and deep scientific specialization ensures both scale and cost efficiency.
China produces the world's most diverse collection of verified botanical species. Based in Changsha, Hunan, MedGence leverages direct geographic links to primary agricultural regions across southwestern and central China. By partnering with Good Agricultural and Collection Practices (GACP) farming cooperatives, we eliminate multi-tier middlemen, secure traceability from field to extraction vat, and reduce freight emissions. This integrated sourcing ensures high active-density harvests while protecting brands from global raw-material bottlenecks.
Many overseas biotech initiatives face long delays when scaling small-scale lab discoveries into commercial runs. MedGence bridges this gap by unifying research benches, intermediate pilot plants, and large-scale industrial manufacturing under one operational system. Our engineering lines handle rapid parameter adjustments, test recovery loops, and refine energy-saving thermal cycles in real time. Clients gain access to agile production schedules, reduced unit costs, and fast delivery timelines across diverse finished dosage forms.
Navigating health authority standards worldwide while maintaining strict intellectual property protection across every stage of contract manufacturing.
Pilot facilities and collaborative production sites adhere strictly to cGMP (21 CFR Part 111 & 211) and ISO 22000 hygiene management frameworks.
Validated testing protocols comply with USP, Ph. Eur., and ChP monographs, covering residual solvents, heavy metals, pesticides, and PAHs.
Client recipes, process parameters, and extraction designs are protected through segregated production lines and binding non-disclosure agreements.
We provide comprehensive documentation support, including Certificates of Analysis (COA), TSE/BSE declarations, and complete export clearances.
Our research, extraction, and standardization services support long-term partnerships with leading public medical centers, academic hospitals, and recognized manufacturers.
 Beijing Tongrentang
 CR Sanjiu
 Sunflower Pharma
 Livzon Pharma
 Dihon Pharma
 Golden Throat
 Yangtzi River Pharma
 Beihai Gofar
 Humanwell Group
 SCIMYTH Pharma
 Shandong Hanfang
 Luoxin Pharma
Straight answers regarding project onboarding, analytical workflows, pilot scale-up, and sustainable manufacturing practices.
Review our contract research services and production modules to help advance your plant-based pipeline smoothly from research to market.
Engage directly with our research scientists and process engineers in Changsha. Whether you need single active screening, chromatographic standard development, or full-scale CDMO manufacturing, we deliver reliable, verifiable outcomes.