Explore our specialized R&D scale-up services, precision analytical workflows, and validated manufacturing programs trusted by industry pioneers worldwide.
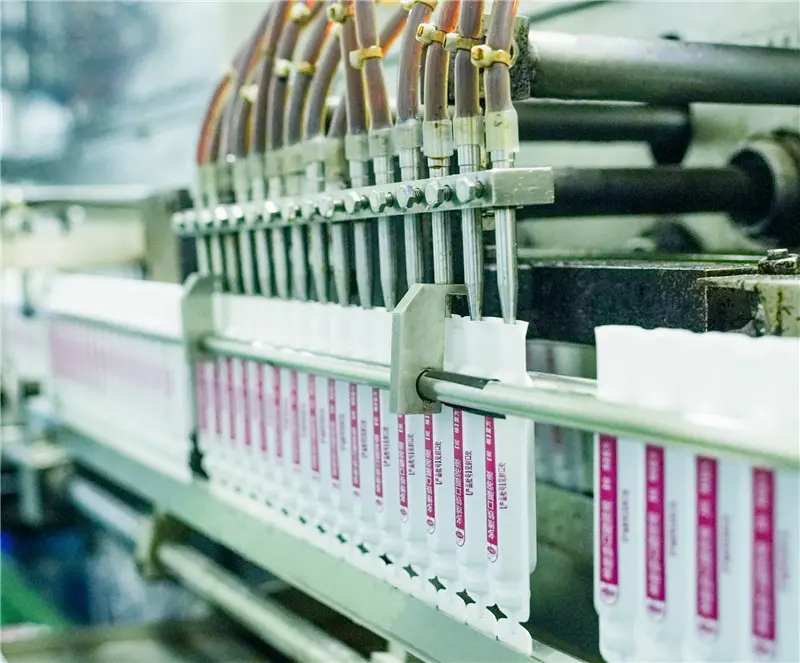
A comprehensive examination of how advanced pilot facilities de-risk bioprocess scale-up, ensure analytical continuity, and streamline international technology transfers.
In the biopharmaceutical and specialized botanical manufacturing industries, bridging the chasm between bench-scale synthesis (milligrams to grams) and commercial-scale production (metric tons) represents the most volatile phase of development. Known across process engineering as the "scale-up valley of death," unpredicted changes in thermodynamic heat dissipation, mass transfer resistance, shear stress, and crystallization kinetics frequently result in compromised product quality, catastrophic batch losses, and regulatory non-compliance.
As a prominent China pilot plant supplier and CDMO, MedGence (Yineng Pharma) operates at the convergence of traditional botanical pharmacopeia and modern bioprocess engineering. Over the past 14+ years, our technical team of more than 300 dedicated research scientists and chemical engineers has successfully modernized 83 classic Traditional Chinese Medicine (TCM) formulas, engineered 22 innovative natural medicine drug candidates, secured 56 hospital preparation registrations, and codified rigorous quality standards for nearly 400 single-herb active pharmaceutical ingredients (APIs).
Whether navigating supercritical CO2 separation for heat-sensitive terpenes, continuous dynamic counter-current extraction of polyphenolic complexes, or macroporous resin adsorption chromatography for high-purity saponins, choosing an authoritative pilot plant partner determines the overall commercial lifecycle and intellectual property exclusivity of therapeutic formulations.
How China's dense industrial synthesis clusters, raw botanical provenance, and engineering capital efficiency benefit global procurement leaders.
China commands over 80% of the world’s indigenous botanical biodiversity for classical medicinal flora. Our strategic location eliminates middlemen, enabling immediate geographic batch tracing, soil mineral verification, and harvest-season synchronization directly at the source.
The fabrication of custom pilot skids—featuring Hastelloy, 316L stainless steel, borosilicate glass systems, and explosion-proof PLC cabinets—proceeds in China at 3x the speed of Western counterparts, slashing lead times from concept to validation.
By leveraging China's integrated supply clusters, clients achieve an estimated 40%–60% reduction in pilot-phase development expenditures without compromising analytical fidelity or international regulatory rigor.
Our pilot plant is structured around modular, interoperable unit operations designed to validate critical process parameters (CPPs) and critical quality attributes (CQAs).
Multi-stage counter-current, ultrasonic-assisted, and heat-reflux extraction systems capable of processing biomass from 50 kg to 500 kg per batch with precise temperature control.
Microfiltration, ultrafiltration, and nanofiltration skids with ceramic and spiral-wound polymeric membranes for molecular weight cut-off fractionation without heat degradation.
Pilot industrial chromatography columns packed with tailored macroporous, ion-exchange, or size-exclusion resins, equipped with automated UV-Vis gradient monitoring.
Falling-film evaporators, wiped-film molecular distillation, freeze dryers (lyophilizers), and spray dryers capable of preserving amorphous crystalline structures.
Fourteen years of rigorous research and manufacturing collaboration with premier national institutes and publicly listed pharmaceutical enterprises.
Stringent adherence to international GMP frameworks, ICH guidelines, and complete confidentiality governance to protect proprietary client assets.
Our pilot plants operate under strict compliance with NMPA GMP, US FDA 21 CFR Part 211, and European Pharmacopoeia (EP) monographs. Complete DQ, IQ, OQ, and PQ documentation accompanies every skid and scale-up campaign.
Every critical process parameter—from column pressure and reflux temperature to flow velocities—is digitally tracked using SCADA architectures compliant with ALCOA+ data integrity principles.
We work exclusively under an entrusted research and manufacturing model. Formulas, process nuances, proprietary fractions, and analytical methods remain client-owned under enforceable bilateral confidentiality covenants.
Transparent technical parameters that define our engineering capacity, solvent compatibility, and processing envelopes.
| Pilot Unit Operation | Working Capacity Range | Wetted Materials | Operational Limits | Integrated PAT / Sensors |
|---|---|---|---|---|
| Dynamic Extraction Skid | 50 L to 1,000 L / batch | SS316L, Hastelloy C-22 | -0.098 MPa to 0.4 MPa, 20°C to 140°C | Inline pH, temp, mass flow, reflux ratio |
| Supercritical CO2 Extractor | 10 L to 100 L vessel | 316Ti forged stainless | Up to 50 MPa, 31°C to 85°C | Coriolis flow meter, co-solvent dosing |
| Membrane Clarification / UF | 100 L/h to 1,500 L/h | Ceramic TiO2/Al2O3, PVDF | Pore sizes: 1 kDa, 5 kDa, 10 kDa, 0.1 µm | Differential pressure transducers, turbidity |
| Industrial Chromatography | Column Ø 200 mm to 800 mm | Borosilicate glass, PTFE | Bed volumes: 20 L to 300 L | Multi-wavelength UV-Vis detector, conductometer |
| Falling-Film Concentration | Evaporation: 50 kg/h to 400 kg/h | Sanitary 316L mirror polish | Vacuum: -0.095 MPa, Temp: 45°C to 75°C | Refractive index Brix probe, level sensors |
| Pilot Spray Dryer Skid | Water evap: 5 kg/h to 35 kg/h | SS304 outer, SS316L contact | Inlet: up to 250°C, Outlet: 70°C to 110°C | Two-fluid nozzle, baghouse DP sensor, humidity |
From botanical drug filings to functional foods and dermal therapeutics, our scale-up recipes directly integrate with regional regulatory filings.
For pharmaceutical entities targeting botanical Investigational New Drug (IND) and New Drug Application (NDA) registrations. We establish identity, impurity profiles, pesticide/heavy-metal limits, and Phase I–IV clinical batches.
Formulators requiring standardized extract ratios (e.g., specific polyphenol or polysaccharide titers) backed by animal and small-group human efficacy data to support substantiated structure/function claims on premium packaging.
Clean-label plant extracts free of toxic solvent residues. Supported by in vitro anti-inflammatory, antioxidant, collagen-synthesis, and transdermal penetration testing suitable for global cosmetic regulatory inventories (INCI).
How the integration of Process Analytical Technology (PAT), Green Chemistry, and continuous flow engineering is revolutionizing botanical extraction.
Moving from post-batch testing to inline real-time release. Utilizing near-infrared (NIR) and Raman spectroscopy to measure critical botanical constituent concentrations dynamically during the extraction and elution cycle.
Replacing large static stirred tanks with continuous counter-current extractors and micro-channel reactors. Continuous flow maximizes mass transfer rates, minimizes thermal exposure times, and guarantees remarkable batch reproducibility.
Pioneering non-flammable, biodegradable natural eutectic solvents to selectively extract poorly soluble flavonoids and polyphenols, entirely eliminating petrochemically derived organic solvent residues from the active fraction.
Our process scale-up dossiers and pilot batches have served the highest echelon of China's medical, pharmaceutical, and scientific research institutions.
 Tongrentang Group
 CR Sanjiu
 Sunflower Pharma
 Livzon Group
 Dihon Pharma
 Golden Throat
 Yangtzi River Pharma
 Beihai Gofar
 Humanwell Healthcare
 SCIMYTH Pharma
 Shandong Hanfang
 Luoxin Pharma
 Zhongsheng Pharma
 Brilliance Herbal
 Apeloa Pharma
 Heng Chang Pharma
 Baotou TCM
 Kamp Medicine
 Guangxi Santo
 Hunan Kangshou
 Jiangxi Juwang
 Beijing Tcmages
 Guizhou Ruihe
 CR Jinchan
 Kangmei Pharma
 Tianjicaotang
 Kingstone Unite
 Shuguang Hospital
 Hunan Direct TCM
 1st Hosp Hunan TCM
 2nd Xiangya Hosp
 2nd Hosp Hunan TCM
 Zhuzhou Orthopedics
Direct technical answers regarding pilot plant validation, minimum batch scales, regulatory audits, and technology transfer dossiers.
Choose an individual research phase or an integrated, full-lifecycle contract development program tailored to your technical timeline.
Speak directly with our senior process engineers and analytical chemists to scope your pilot trial parameters, tech transfer roadmap, or custom skid manufacturing requirements.