Industrial botanical actives, bio-potency evaluations, and end-to-end clinical trial development engineered to cGMP, USP, and Ph. Eur. international compendial standards.
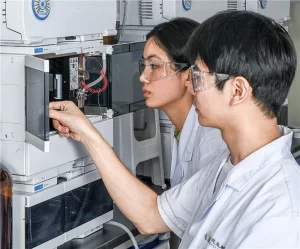
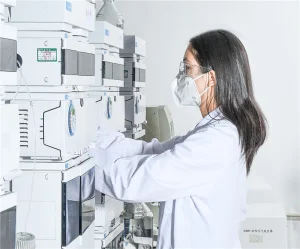
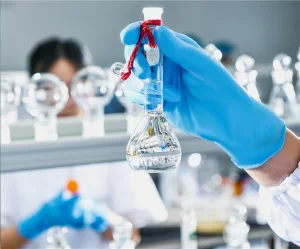
Transitioning from crude, inconsistent herbal decoctions to quantified, molecular-targeted therapeutic solutions through integrated CRO/CDMO services in Changsha, Hunan.
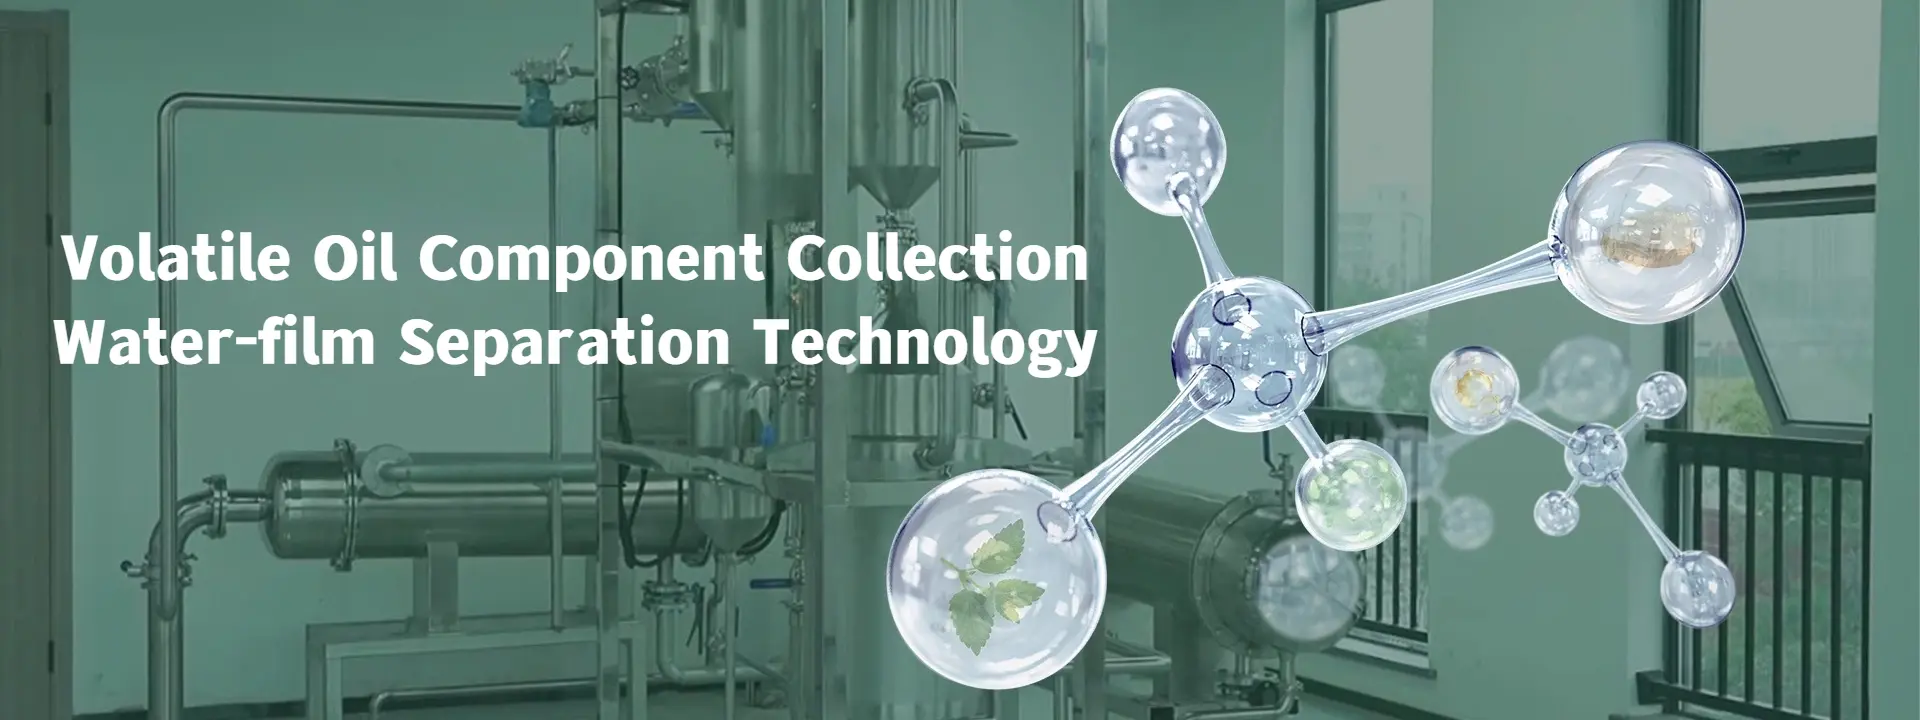
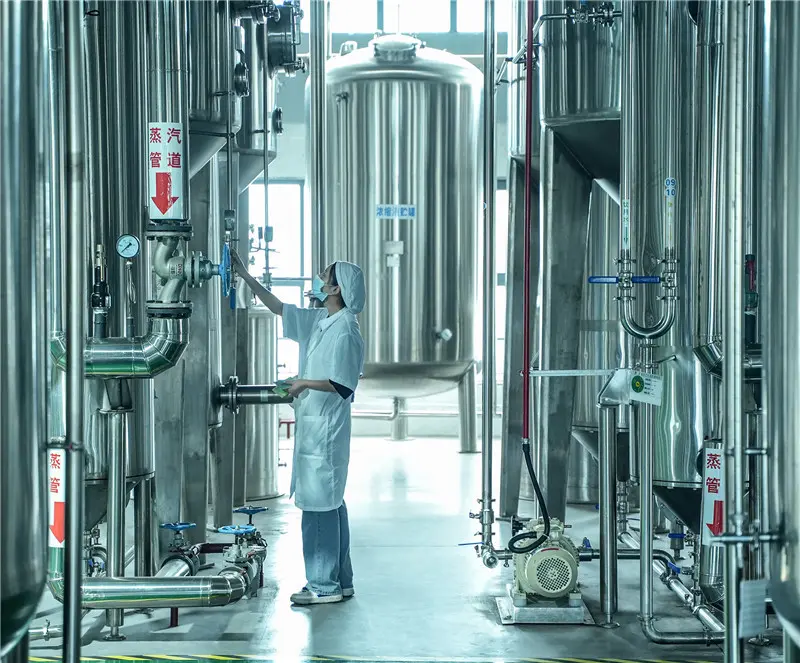
Traditional thermal evaporation degrades thermolabile polyphenols, volatile terpenes, and active glycosides. MedGence employs modern Low-Temperature Vacuum Membrane Evaporation and centrifugal film concentration down to 35°C, ensuring the full bioactive spectrum remains intact.
Achieving pharmaceutical-grade botanical concentrates demands more than liquid-to-solid ratio reduction. We combine macroporous adsorption resin columns, continuous countercurrent extraction, and preparative chromatography to enrich active fraction purity up to 98% while stripping residual heavy metals and agrochemicals.
Validated with HPLC, GC-MS, and HPTLC high-resolution fingerprinting, every batch delivers consistent batch-to-batch chemical equivalence. We overcome regional, harvest-season, and plant-part variations to supply stable botanical concentrates ready for multi-center clinical pipelines.
How state-of-the-art closed-loop synthesis, AI-guided PAT monitoring, and sustainable raw material backward-integration establish an unshakeable commercial supply bridge.
Inline near-infrared (NIR) sensors track active compound mass transfer during continuous concentration cycles, eliminating batch deviations before they occur.
Automated vacuum recovery systems capture and distill >95% of ethanol, ethyl acetate, and acetone solvents, driving down carbon emissions and production unit costs.
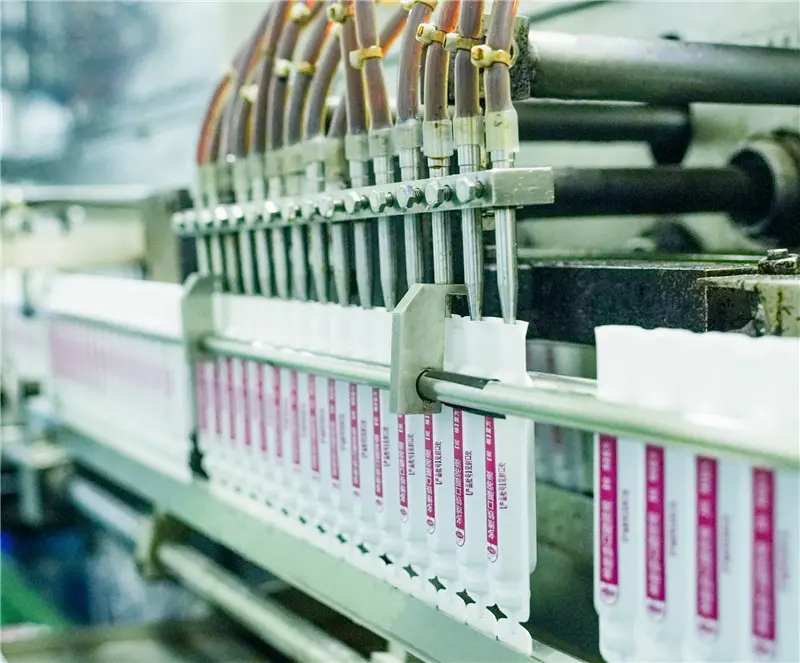
Hermetically sealed pharmaceutical-grade lines certified under Class D cleanrooms guarantee clean extracts free of environmental micro-particulates, endotoxins, and PAH residues.
Seamless technological handoff from benchtop glass distillation (100 mL) to pilot runs (50 L) and multi-ton industrial falling-film concentration plants without thermal drift.
Addressing the specific regulatory, functional, and commercial pain points experienced by enterprise formulators across North America, Europe, and Asia-Pacific.
Complete eCTD-ready Module 3 Chemistry, Manufacturing, and Controls (CMC) dossiers, including validated analytical method transfers, stability protocols (ICH Q1A), and comprehensive Phase I-IV clinical data packets.
High-density, highly water-dispersible botanical concentrate powders and liquids calibrated for bioavailability. Full compliance with FSMA, FDA 21 CFR 111, EFSA novel food criteria, and clean-label non-GMO standards.
Cellular-level antioxidant, anti-glycation, and anti-inflammatory assays. Odor-mitigated, clarified botanical concentrates engineered for optimal dermal absorption without altering finished cosmetic base color or stability.
Supplying validated botanical active concentrates and CRO research services to industry pioneers across greater China and international healthcare systems.
 China Beijing Tongrentang Group
 China Resources Sanjiu Medical & Pharma
 Sunflower Pharmaceutical Group
 Livzon Pharmaceutical Group
 Dihon Pharmaceutical Group
 Golden Throat Holdings Group
 Yangtzi River Pharmaceutical Group
 Humanwell Healthcare Group
Continuous investment in artificial intelligence, molecular modeling, and green supercritical fluid engineering defines our strategic vision for the next decade.
Accelerating botanical active screening through computer-aided network pharmacology. Our database cross-references hundreds of thousands of research batches against key biological targets, shortening discovery cycles from years to months.
Replacing traditional organic solvents with supercritical carbon dioxide and environmentally clean subcritical water extraction systems, ensuring non-toxic, clean-label processing for infant nutrition and sterile pharma formulas.
Developing liposomal and self-emulsifying drug delivery systems (SEDDS) for hydrophobic botanical concentrates (e.g., curcuminoids, berberine, and apigenin), multiplying human plasma bioavailability up to 15-fold.
Essential guidance covering regulatory documentation, confidential IP protection, quality standards, and CDMO contract supply workflows.
Unlike raw ingredient aggregators, MedGence operates as a fully integrated CRO and CDMO. We pair high-throughput pilot-to-scale concentration facilities with in-house analytical laboratories (HPLC, HPTLC, GC-MS), proprietary safety testing (LD50, acute/chronic toxicology), and multi-phase clinical validation, providing a complete turnkey transfer path.
All contract development and custom manufacturing partnerships operate under strict mutual Non-Disclosure Agreements (NDAs). Detailed parameter matrices, solvent ratios, and clinical findings are sequestered in enterprise-grade secured networks, ensuring our global clients preserve undisputed commercial exclusivity.
We supply raw active materials as highly clarified concentrated liquids, flowable extract powders, viscous pharmaceutical pastes, or volatile essential oils. Finished product contract packaging covers oral liquids, hard-shell capsules, softgels, tablets, effervescent granules, and micro-pellets.
Our scientific team evaluates botanical raw materials sampled across multiple provinces and growing seasons. We characterize chemical shifts using chromatographic fingerprinting and adjust extraction parameters to ensure finished concentrates maintain constant active potency across production campaigns.
Directly managed contract manufacturing services designed to transition proven clinical studies into market-ready finished formulations.